Sand Casting Procedure Steps: A Complete Practical Guide
Welcome to My Blog!
I’m thrilled to have you here! Before we dive into the content, I’d love for you to join me on my social media platforms. It’s where I share extra insights, connect with our amazing community, and keep you updated on the latest news. Here’s how you can stay connected:
📘 Facebook: Shanghai Leierwo Industry Trade Co., Ltd.
Now, let’s embark on this journey together! I hope you find the content here not only insightful but also inspiring and valuable. Let’s get started!
Table of Contents
- Master the full sand casting procedure from raw material to finished part
- Learn step-by-step sand casting workflow used in real foundries
- Understand key parameters, standards, and process control methods
- Explore defects, quality inspection, and improvement strategies
- Compare sand casting with other casting processes for better selection
- Discover real-world case studies and industry applications
- Get practical answers to conversational, search-driven questions
Introduction
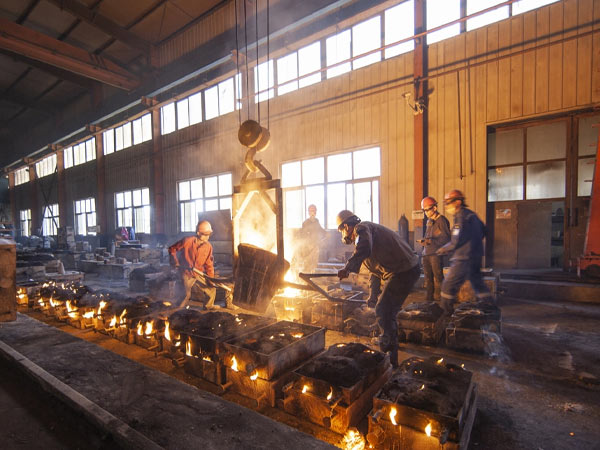
In today’s highly advanced manufacturing landscape—where CNC machining, additive manufacturing, and automated production lines are rapidly evolving—the sand casting procedure remains one of the most widely used and trusted metal forming processes worldwide.
According to industry reports, sand casting accounts for over 60% of all metal casting production globally, especially in sectors like automotive, heavy machinery, and infrastructure. Its adaptability to complex geometries, wide material compatibility, and low tooling cost make it indispensable for both prototyping and large-scale production.
If you are exploring sourcing options or evaluating manufacturing methods, understanding the sand casting procedure steps is essential. It not only helps in cost control but also improves communication with suppliers and ensures product quality meets engineering requirements.
Overview of Sand Casting Procedure
The sand casting procedure is a manufacturing process in which molten metal is poured into a sand mold cavity and allowed to solidify into the desired shape.
The process involves several sequential steps:
- Pattern creation
- Mold preparation
- Core placement
- Metal melting and pouring
- Cooling and solidification
- Shakeout and finishing
Each step plays a critical role in determining the final casting quality.
Sand Casting Procedure Steps Explained in Detail
Pattern Making in Sand Casting Procedure
Purpose of Pattern Design
A pattern is a physical model used to form the mold cavity. It is typically made slightly larger than the final product to compensate for shrinkage during cooling.
Patterns can be made from wood, plastic, aluminum, or steel depending on production volume and precision requirements.
Allowances in Pattern Making
Pattern design includes:
- Shrinkage allowance (typically 1–3%)
- Machining allowance
- Draft angles for easy removal
These considerations ensure dimensional accuracy and manufacturability.
Mold Preparation in Sand Casting Procedure
Sand Composition and Properties
Molding sand typically consists of:
- 85–95% silica sand
- 5–10% clay (binder)
- 2–5% water
This mixture provides:
- Strength to hold shape
- Permeability for gas escape
- Refractoriness to withstand high temperatures
Mold Formation Process
The sand is packed around the pattern in a molding box. Once compacted, the pattern is removed, leaving a cavity.
This cavity defines the external geometry of the casting.
Core Making for Internal Structures
Role of Cores in Sand Casting Procedure
Cores are used to create hollow sections or internal cavities in castings.
They are made from specially bonded sand mixtures to ensure strength during pouring.
Core Placement Accuracy
Proper positioning of cores is critical. Misalignment can result in dimensional defects or weak structures.
Gating System Design
Function of Gating System
The gating system controls how molten metal flows into the mold. It includes:
- Sprue
- Runner
- Gate
A well-designed gating system minimizes turbulence and prevents defects.
Risers and Feeding Systems
Risers act as reservoirs of molten metal to compensate for shrinkage during solidification.
This ensures the casting remains dense and free of voids.
Metal Melting and Pouring
Furnace Types and Temperature Control
Common furnaces include:
- Induction furnaces
- Electric arc furnaces
- Cupola furnaces
Temperature ranges vary by material:
- Aluminum: 660–750°C
- Cast iron: 1150–1300°C
- Steel: 1500–1600°C
Precise temperature control ensures proper fluidity and reduces defects.
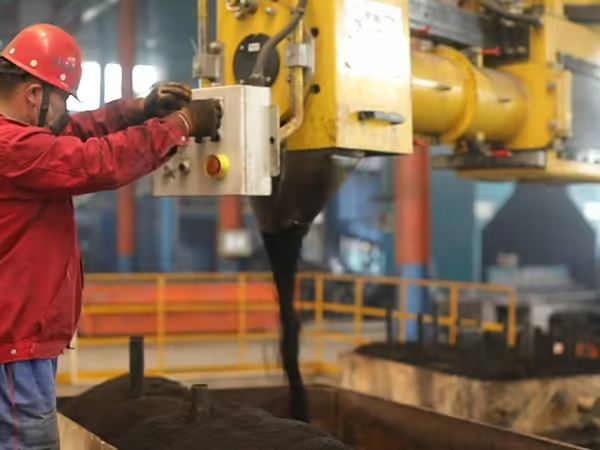
Pouring Techniques
Molten metal must be poured smoothly to avoid:
- Air entrapment
- Oxidation
- Turbulence
Proper pouring improves casting integrity.
Cooling and Solidification Behavior
Solidification Dynamics
Cooling rate influences:
- Grain structure
- Mechanical strength
- Internal stress
Slow cooling results in coarse grains, while rapid cooling produces finer microstructures.
Directional Solidification
Engineers design molds to ensure metal solidifies progressively from one end to another, reducing shrinkage defects.
Shakeout and Casting Extraction
Mold Breakdown Process
After solidification, the sand mold is broken to remove the casting. This is known as shakeout.
The sand can often be recycled after processing.
Cleaning, Fettling, and Finishing
Removal of Excess Material
Gates, risers, and flash are removed using cutting or grinding.
Surface Treatment
Common finishing processes include:
- Shot blasting
- Sandblasting
- Machining
These steps improve surface quality and dimensional accuracy.
Key Process Parameters in Sand Casting Procedure
| Parameter | Typical Value Range | Impact on Casting Quality |
|---|---|---|
| Pouring Temperature | 660–1600°C | Affects flow and defect formation |
| Sand Grain Size | 0.1–1 mm | Determines surface finish |
| Moisture Content | 2–8% | Influences mold strength |
| Cooling Rate | Variable | Controls microstructure |
| Shrinkage Allowance | 1–3% | Ensures dimensional accuracy |
Advantages of Sand Casting Procedure
High Versatility
The process supports a wide range of metals, including iron, steel, aluminum, and copper alloys.
Cost Efficiency
Tooling costs are relatively low, making it suitable for both small and large production runs.
Scalability
Sand casting can produce components ranging from a few grams to several tons.
Limitations of Sand Casting Procedure
Surface Roughness
Compared to precision casting methods, sand casting produces rougher surfaces.
Lower Dimensional Accuracy
Tolerances are wider, requiring secondary machining in some cases.
Sand Casting vs Other Casting Methods
Sand Casting vs Die Casting
- Sand casting: lower cost, flexible
- Die casting: high precision, high volume
Sand Casting vs Investment Casting
- Sand casting: suitable for large parts
- Investment casting: superior surface finish
Sand Casting vs Permanent Mold Casting
- Sand molds are disposable
- Permanent molds improve consistency
Industry Standards and Quality Control
Common Standards
- ASTM A48: Gray iron castings
- ASTM A27: Steel castings
- ISO 8062: Dimensional tolerances
These standards ensure consistency and reliability across global supply chains.
Inspection Methods
Quality control includes:
- Visual inspection
- Ultrasonic testing
- X-ray inspection
- Dimensional measurement
Common Defects and Prevention
Gas Porosity
Caused by trapped gases. Prevented by improving mold permeability and venting.
Shrinkage Cavities
Reduced by proper riser design and directional solidification.
Sand Inclusion
Avoided through proper mold preparation and cleaning.
Real-World Case Studies
Automotive Engine Block Production
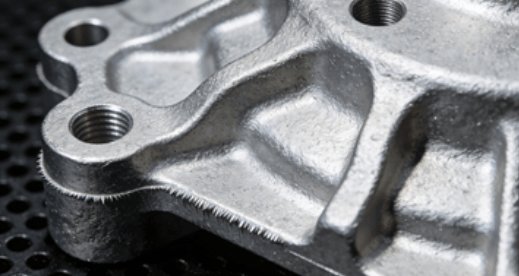
Sand casting is widely used for engine blocks due to its ability to produce complex internal geometries.
Manufacturers achieve:
- High strength
- Cost efficiency
- Scalable production
Heavy Machinery Components
Large components like pump housings and valve bodies are produced using sand casting due to size flexibility.
Emerging Trends in Sand Casting
Automation in Foundries
Modern foundries use robotic systems for:
- Mold handling
- Pouring
- Finishing
This improves efficiency and consistency.
Sustainable Casting Practices
Recycling sand and reducing emissions are key focus areas in modern manufacturing.
FAQ
What are the steps in the sand casting procedure?
The process includes pattern making, mold preparation, core placement, melting, pouring, cooling, shakeout, and finishing. Each step ensures casting quality and accuracy.
Why is sand casting widely used?
It is cost-effective, flexible, and suitable for a wide range of metals and sizes. It is ideal for both prototypes and large-scale production.
How accurate is sand casting?
It offers moderate accuracy compared to other casting methods. Secondary machining is often required for tight tolerances.
What industries use sand casting?
Industries include automotive, construction, energy, and heavy machinery manufacturing.
Can sand casting produce complex shapes?
Yes, especially with the use of cores, sand casting can create intricate internal and external geometries.
Conclusion
The sand casting procedure continues to be a foundational manufacturing method due to its flexibility, cost efficiency, and wide applicability. By understanding each step and the factors influencing quality, manufacturers and buyers can make informed decisions that improve performance and reduce costs.
Whether you are sourcing components or optimizing production, mastering the sand casting procedure steps is essential for achieving consistent and high-quality results in modern industry.
Product Categories
- Valve Parts
- Water Pump Parts
- Bearing Box Parts
- Die Casting Parts
- Stainless Steel Pump Products
- Cast Iron Pump Products
- Valve Parts For Automobile Use
- Auto Parts
- Valve Parts For Civil Use
- Vacuum Pump Parts KF

Let’s start your next project!
Start Your Project with Leierwo
1. Submit Your Inquiry
2. Cost Calculation
3. Start Production
4. Arrange Delivery
FAQ
Yes, we have extensive experience in international trade and can assist customers with export customs clearance and shipping arrangements. We offer various trade terms such as FOB, CIF, and DDP to accommodate different logistics needs.We accept various international payment methods, including T/T (Telegraphic Transfer), wire transfer, and Letter of Credit (L/C). Payment terms can be discussed with our sales team.
By partnering with Leierwo, you can enjoy competitive pricing and superior quality compared to other suppliers. Additionally, we offer a one-stop solution to deliver finished parts, including CNC machining and surface treatment, ensuring a seamless production process.
We have advanced casting equipment and strict quality control systems. Our monthly production capacity is substantial, and we can manufacture products based on customer-provided drawings or samples. We accept both small trial orders and large-scale production.
Our products comply with international standards such as ASTM, AISI, DIN, and JIS. We can provide material test reports and relevant certifications to ensure product quality meets customer requirements.
We strictly follow the ISO 9001 quality management system and conduct multiple inspections throughout the production process, including spectrographic analysis, X-ray testing, ultrasonic testing, and dimensional measurements. These quality control measures guarantee that our castings meet the highest standards.
Our MOQ depends on the product type and complexity, However, we are flexible and open to discussing your specific needs.
Our standard production lead time is 4-6 weeks, depending on order quantity and product complexity. We strive to shorten delivery times to meet customer demands.
Yes, we can provide samples for quality inspection. Sample costs and shipping fees can be negotiated, and sample fees may be refunded upon placing a formal order.
 English
 Spanish
 Arabic
 Malay
 German