Pump Impeller: Datum and Runout Requirements for Cast Blanks
Table of Contents
For buyers reviewing pump impeller, a useful specification connects the service, the approved drawing and the delivered component. This guide examines the purchasing question “Datum and Runout Requirements for Cast Blanks”. Use it to organize the supplier discussion before approving material, tooling or production.
Key purchasing decisions for pump impeller
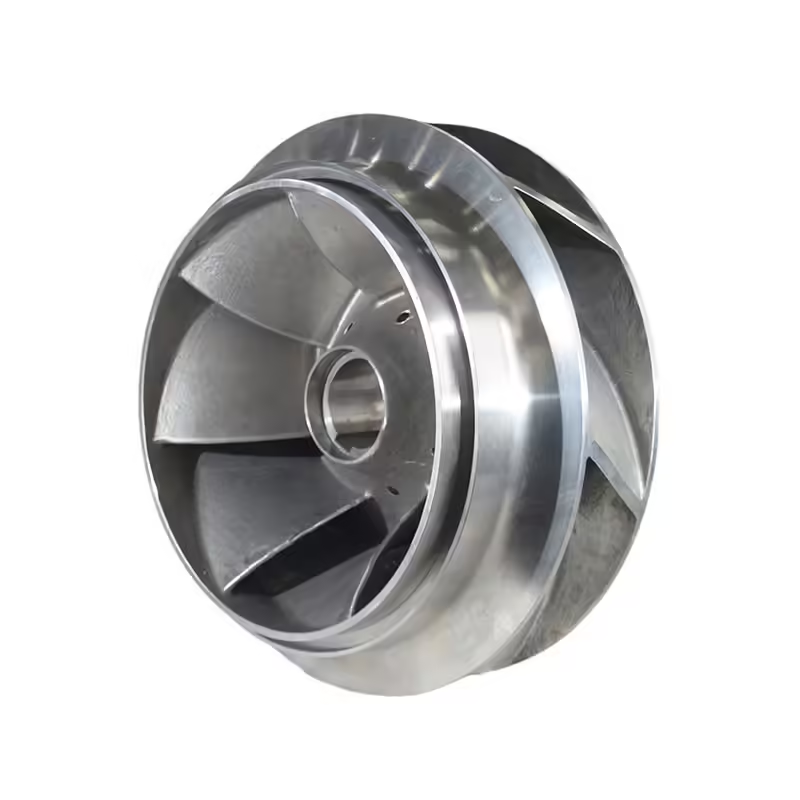
A pump impeller needs a consistent datum scheme so casting, machining and inspection refer to the same geometry. The shaft bore, shrouds and wear interfaces cannot be controlled reliably by unrelated measurements. Define the final rotational reference before the blank is manufactured.
Review the design and interfaces
Mark the functional axis and axial reference face on the drawing. Allocate machining stock to the bore and mating faces. Ask the foundry and machine shop to review how the raw casting will be located during first setup.
Compare the purchasing options
Use this comparison when reviewing pump impeller against a controlled drawing and purchase specification.
| Purchasing approach | Main implication | What to resolve |
|---|---|---|
| Independent feature checks | May miss relationships | Does not establish rotational alignment |
| Functional datum inspection | Controls related geometry | Use the final machining references |
Select the manufacturing route
Compare investment casting, sand casting or another feasible route using the actual part rather than its outer diameter alone. Passage access, core work, finishing and batch size can dominate the decision. Request the same delivered condition and inspection scope from every bidder.
For a project involving pump impeller, compare the complete delivered condition before choosing a production route.
Inspection requirements for pump impeller
Inspect runout and related dimensions from the approved datums after finish machining. Keep raw-casting variation separate from finished-part tolerance. Document any deviation before balancing or assembly work proceeds.
Apply the review to a practical case
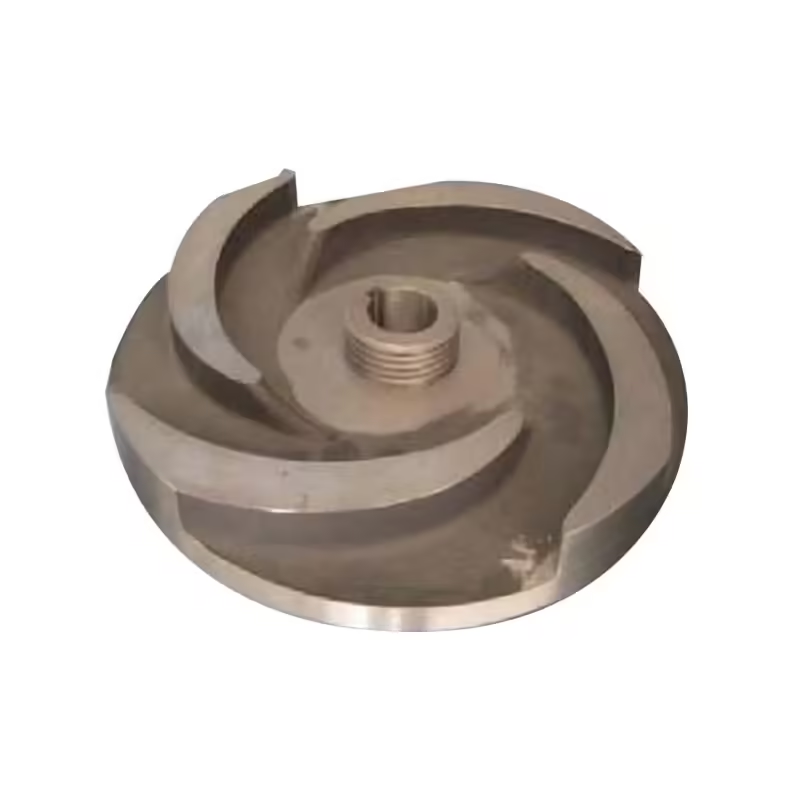
A rotor may have acceptable individual diameters yet show excessive runout because its features were machined from inconsistent setups. A shared datum plan helps prevent that mismatch before production.
Define a complete quotation scope
Provide the approved component drawing, material, rotation where relevant, shaft or casing interfaces, operating fluid and quantities. State the machining and inspection scope, including the specified balance configuration for rotating parts. Keep complete pump performance validation assigned to the appropriate equipment-level plan.
When discussing pump impeller, separate requirements already approved by engineering from options still awaiting review.
For background reading, see Hydraulic Institute pump principles and impeller reference. Use the applicable project specification and approved design for contractual requirements.
Discuss the component with Leierwo
Review Leierwo’s Pump Manufacturing and Investment Casting pages, then send the controlled drawing, material and quantity for a component-specific discussion. Ask the quotation to state the manufacturing scope, inspection evidence and any proposed alternatives.
A request concerning pump impeller should lead to a part-specific quotation, with assumptions and deviations stated in writing.
Frequently asked questions
What is the main buying issue with pump impeller?
A pump impeller needs a consistent datum scheme so casting, machining and inspection refer to the same geometry. The shaft bore, shrouds and wear interfaces cannot be controlled reliably by unrelated measurements.
Which design details should be included?
Mark the functional axis and axial reference face on the drawing. Allocate machining stock to the bore and mating faces.
What should inspection cover when evaluating pump impeller?
Inspect runout and related dimensions from the approved datums after finish machining. Keep raw-casting variation separate from finished-part tolerance.
How should the purchasing options be compared?
Compare “Independent feature checks” and “Functional datum inspection” against the same finished-part requirements. Key review points are “does not establish rotational alignment” and “use the final machining references”, respectively.
What should an inquiry about pump impeller include?
Send the pump and part identification, approved drawing, material, duty information, interfaces and final machining or balancing requirements.
Product Categories
- Valve Parts
- Water Pump Parts
- Bearing Box Parts
- Die Casting Parts
- Stainless Steel Pump Products
- Cast Iron Pump Products
- Valve Parts For Automobile Use
- Auto Parts
- Valve Parts For Civil Use
- Vacuum Pump Parts KF

Let’s start your next project!
Start Your Project with Leierwo
1. Submit Your Inquiry
2. Cost Calculation
3. Start Production
4. Arrange Delivery
FAQ
Yes, we have extensive experience in international trade and can assist customers with export customs clearance and shipping arrangements. We offer various trade terms such as FOB, CIF, and DDP to accommodate different logistics needs.We accept various international payment methods, including T/T (Telegraphic Transfer), wire transfer, and Letter of Credit (L/C). Payment terms can be discussed with our sales team.
By partnering with Leierwo, you can enjoy competitive pricing and superior quality compared to other suppliers. Additionally, we offer a one-stop solution to deliver finished parts, including CNC machining and surface treatment, ensuring a seamless production process.
We have advanced casting equipment and strict quality control systems. Our monthly production capacity is substantial, and we can manufacture products based on customer-provided drawings or samples. We accept both small trial orders and large-scale production.
Our products comply with international standards such as ASTM, AISI, DIN, and JIS. We can provide material test reports and relevant certifications to ensure product quality meets customer requirements.
We strictly follow the ISO 9001 quality management system and conduct multiple inspections throughout the production process, including spectrographic analysis, X-ray testing, ultrasonic testing, and dimensional measurements. These quality control measures guarantee that our castings meet the highest standards.
Our MOQ depends on the product type and complexity, However, we are flexible and open to discussing your specific needs.
Our standard production lead time is 4-6 weeks, depending on order quantity and product complexity. We strive to shorten delivery times to meet customer demands.
Yes, we can provide samples for quality inspection. Sample costs and shipping fees can be negotiated, and sample fees may be refunded upon placing a formal order.
 English
 Spanish
 Arabic
 Malay
 German