Investment Casting Cost Factors Explained
Table of Contents
Introduction
Investment casting cost is influenced by far more than the weight of the finished metal component. For OEM buyers, engineers and procurement teams, a reliable quotation must consider tooling, material grade, part geometry, casting process, tolerance requirements, surface finish, heat treatment, CNC machining, inspection and expected production volume.
This is why two components with similar dimensions can have very different manufacturing requirements.
A relatively simple carbon steel machinery component produced through water glass casting may follow a very different cost structure from a stainless steel precision component requiring silica sol casting, tight dimensional control, CNC machining and additional inspection.
Leierwo provides investment casting services covering water glass and silica sol processes, multiple material families, structural optimization, tooling, trial production, machining and quality inspection. Understanding how these stages affect the complete manufacturing route helps buyers evaluate quotations more accurately rather than focusing only on the unit value of the raw casting.
What Determines Investment Casting Cost?
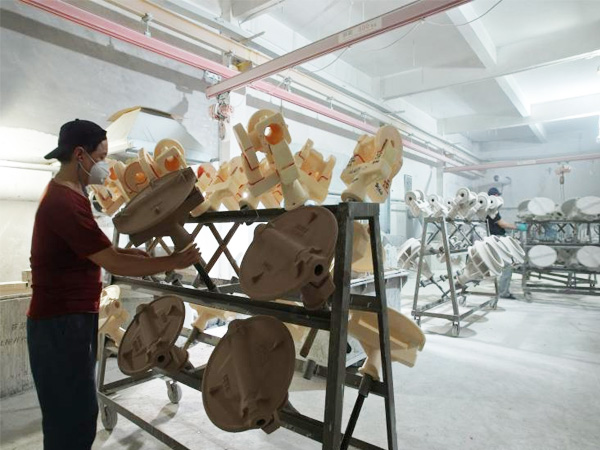
Investment casting cost is normally the result of several connected manufacturing decisions.
The most important variables include component geometry, material, casting method, tooling complexity, component weight, production quantity, tolerance, surface finish, heat treatment, machining and inspection.
These variables also influence one another.
For example, requiring a tighter tolerance may lead to silica sol casting instead of water glass casting. It may also require more inspection or additional CNC machining.
Likewise, selecting a difficult-to-machine alloy can affect both raw material requirements and downstream machining effort.
A meaningful cost evaluation therefore needs to look at the entire production route.
Part Geometry and Complexity
Geometry is one of the first factors a casting manufacturer evaluates.
Investment casting is particularly valuable because it can reproduce complex structures such as thin walls, internal cavities, curved surfaces and irregular shapes.
Leierwo specifically supports customization from 3D drawings, CAD models and physical samples, including components with thin walls, internal cavities and special geometries.
However, greater complexity usually requires more engineering work.
A component containing complicated internal cavities may require additional tooling features, more careful wax pattern control and a more sophisticated gating system.
Highly asymmetrical components can also be more difficult to arrange efficiently on a casting tree.
The key question is therefore not whether a design is complex, but whether every feature is functionally necessary.
Simplifying unnecessary geometry before tooling begins can reduce manufacturing difficulty without changing product performance.
Tooling Complexity
Investment casting usually requires tooling to create repeatable wax patterns.
Tooling design depends on the geometry of the component.
A relatively simple part may use straightforward tooling, while complicated shapes can require:
- Multiple tool sections
- Inserts
- Slides
- Complex parting arrangements
- Additional dimensional control
Tooling represents an initial project investment rather than only a per-part manufacturing activity.
This means production quantity becomes important.
If the tooling supports thousands of components over the life of a project, its contribution to each part becomes relatively small. For very small production quantities, the same tooling investment is distributed across fewer components.
Leierwo’s process includes mold development, mold trials and dimensional calibration before repeat casting production begins.
Water Glass vs Silica Sol Casting
One of the most important process choices affecting investment casting cost is whether the project uses water glass or silica sol casting.
Leierwo currently offers both processes.
Water glass casting typically provides approximately CT7–CT8 dimensional capability with surface roughness around Ra 12.5.
Silica sol casting can reach approximately CT4–CT6 with surface roughness around Ra 6.3.
| Factor | Water Glass Casting | Silica Sol Casting |
|---|---|---|
| Typical accuracy | CT7–CT8 | CT4–CT6 |
| Typical surface roughness | Around Ra 12.5 | Around Ra 6.3 |
| Typical application | Machinery and structural parts | Higher-precision components |
| Process positioning | Functional and economical | Higher precision and finish |
| Secondary processing | May require more finishing | Can reduce some finishing |
The most precise process is not automatically the best choice.
If a component will later undergo extensive CNC machining, paying for tighter as-cast tolerance on every surface may provide little additional value.
Leierwo’s own investment casting guidance positions water glass casting for applications such as excavator and agricultural machinery components, while silica sol casting is used where higher dimensional accuracy and surface quality are required.
Material Grade
Material is another major influence on investment casting cost.
Leierwo supports more than 40 casting materials across stainless steel, carbon steel, alloy steel, aluminum and other engineering alloys.
Different materials have different:
- Raw material requirements
- Melting behavior
- Pouring temperatures
- Heat-treatment needs
- Machining characteristics
- Inspection requirements
Carbon steel is often suitable for general machinery applications where corrosion resistance is not the primary requirement.
Stainless steel may be selected for pumps, valves and components exposed to moisture or chemicals.
Alloy steel may be required where higher strength, fatigue resistance or wear performance is needed.
The correct approach is to select the material according to service conditions rather than simply choosing the highest-performing alloy available.
Stainless Steel Casting Requirements
Stainless steel can increase manufacturing complexity because certain grades require tighter composition control, specific heat treatment and different machining strategies.
If the application genuinely requires corrosion resistance, this additional effort creates functional value.
If the component operates in a protected mechanical environment, however, a simpler material may be sufficient.
Leierwo supports multiple stainless steel grades through its investment casting process and also provides dedicated stainless steel casting solutions.
Buyers should therefore define the operating environment before finalizing the alloy.
Alloy Steel Requirements
Alloy steels such as 42CrMo can be used where higher mechanical performance is required.
These materials may also involve additional heat treatment or harder machining conditions.
This means the finished component should be evaluated as more than the raw casting.
A high-strength alloy may require:
- Controlled thermal processing
- Hardness verification
- Additional machining effort
- More specific mechanical requirements
The material should only be upgraded where the application benefits from those properties.
Finished Component Weight
Component weight affects the amount of metal required, but the relationship is not based only on finished net weight.
The foundry must also consider the metal used in:
- Runners
- Gates
- Sprues
- Feeding systems
The total poured metal can therefore be greater than the weight of the final component.
This relationship is often described through casting yield.
Improving yield means producing more finished component weight from the same amount of poured metal.
Good gating and tree design can therefore influence both manufacturing stability and material efficiency.
Casting Yield
Casting yield becomes particularly important in repeat production.
If a component requires a large feeding system relative to its finished weight, more metal must be melted and handled for each acceptable part.
A more efficient tree layout can improve material utilization, but yield cannot be maximized at the expense of quality.
Insufficient feeding may increase the risk of shrinkage or incomplete filling.
The engineering objective is therefore to find a stable balance between material utilization and process reliability.
Production Volume
Quantity changes the economics of investment casting significantly.
Tooling, engineering, process setup and fixture development are largely initial or semi-fixed activities.
As volume increases, these activities can be distributed across more components.
Leierwo supports production ranging from single-piece trials and small batches through repeat and mass production.
For buyers, both order quantity and expected annual quantity should therefore be provided.
A project requiring 100 pieces once is different from one requiring 100 pieces every month for several years.
The supplier may design tooling, fixtures and production planning differently when long-term demand is known.
Prototype vs Repeat Production
Prototype quantities often involve a higher amount of engineering work relative to the number of components produced.
The first production stage may include:
- Drawing review
- Tool development
- Sample manufacturing
- Dimensional verification
- Process adjustment
Repeat production benefits from an already-developed process.
Fixtures, inspection methods and manufacturing parameters have usually been validated.
Leierwo’s manufacturing workflow includes initial sample production and approval before full production, allowing the component and process to be confirmed before larger quantities are manufactured.
This is why buyers should distinguish clearly between prototype requirements and expected production demand.
Dimensional Tolerance
Tolerance can have a major impact on manufacturing complexity.
Investment casting already provides relatively strong dimensional capability, but not every dimension should be assigned the tightest possible tolerance.
The more demanding the tolerance, the more attention may be required in:
- Tooling
- Wax control
- Casting process
- Inspection
- Straightening
- CNC machining
Leierwo’s silica sol process provides tighter typical dimensional capability than its water glass process, making it suitable for higher-precision applications.
However, engineering drawings should clearly distinguish critical and non-critical dimensions.
Avoid Over-Tolerancing
Over-tolerancing is one of the easiest ways to add unnecessary manufacturing complexity.
Suppose a cast housing contains 30 dimensions, but only five determine assembly, sealing or alignment.
Applying precision-level tolerance to all 30 dimensions provides little practical benefit.
Instead, the drawing should identify features such as:
- Bearing positions
- Sealing interfaces
- Mating diameters
- Mounting points
- Alignment features
These areas can receive tighter control or machining.
Less critical surfaces can remain within practical casting tolerances.
This approach helps maintain performance while avoiding unnecessary processing.
Surface Roughness
Surface requirements also affect the manufacturing route.
Leierwo reports typical surface roughness of approximately Ra 12.5 for water glass casting and Ra 6.3 for silica sol casting.
If a component requires a smoother surface throughout, silica sol casting may reduce the amount of grinding or polishing required later.
However, there is little reason to specify very fine surface quality on areas that are hidden, non-functional or later machined.
The surface requirement should be matched to the application.
CNC Machining Requirements
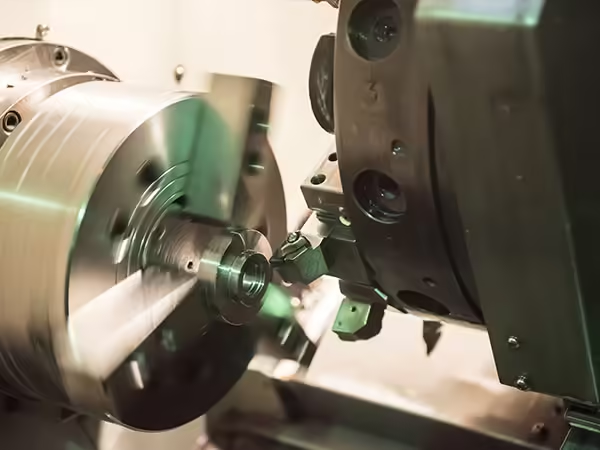
Investment casting is often described as a near-net-shape process, but many industrial components still require precision machining.
Common machined features include:
- Bearing seats
- Threads
- Precision bores
- Sealing faces
- Mounting surfaces
- Mating diameters
The amount of machining can significantly affect the total manufacturing effort.
Leierwo combines investment casting with CNC machining services and specifically evaluates Design for Manufacturability and production optimization before full-scale manufacturing.
This allows casting and machining to be planned as one process instead of quoting them as unrelated stages.
Machining Allowance
Machining allowance is the additional metal deliberately left on a cast surface so it can later be machined to final size.
Too little allowance can create problems if the casting varies slightly and does not contain enough material for final finishing.
Too much allowance increases machining effort.
The correct value depends on:
- Component size
- Casting method
- Material
- Expected distortion
- Final tolerance
- Surface condition
Machining allowance should therefore be determined feature by feature rather than simply adding excess metal to the entire component.
Heat Treatment
Many cast metals require heat treatment to achieve their final mechanical properties.
Leierwo’s production workflow includes treatments such as solution treatment and tempering according to material requirements before precision finishing.
Heat treatment may be needed to develop:
- Strength
- Hardness
- Toughness
- Wear resistance
- Dimensional stability
Different alloys require different thermal processes.
This is particularly important for alloy steels and precipitation-hardening materials.
The heat-treatment condition should therefore be included in the RFQ where mechanical performance is critical.
Surface Treatment
A finished investment casting may also require surface treatment.
Depending on the application, this can include:
- Shot blasting
- Sandblasting
- Polishing
- Passivation
- Painting
- Plating
- Protective coating
Each additional operation adds processing stages.
The required finish should therefore be based on function and environmental exposure rather than appearance alone.
A pump component exposed to corrosive fluid has very different surface requirements from an internal machinery bracket.
Inspection Requirements
Inspection requirements can vary dramatically from one project to another.
A general machinery component may require basic dimensional and material verification.
A more critical component may require:
- Full dimensional inspection
- Spectral analysis
- Penetrant testing
- Ultrasonic testing
- Mechanical testing
- Additional documentation
Leierwo’s manufacturing workflow includes raw-material analysis, dimensional measurement and non-destructive testing such as PT and UT where required.
Inspection should reflect functional risk.
Requesting extensive inspection for every non-critical feature can increase manufacturing effort without improving actual product performance.
Quality Requirements and Documentation
Some projects require more documentation than others.
Buyers may request:
- Material certificates
- Inspection reports
- Dimensional records
- Process records
- Heat-treatment documentation
These requirements should be stated before quotation.
Changing inspection or documentation expectations after production has begun can create delays or require additional testing.
A complete RFQ helps both sides establish the correct quality plan from the beginning.
Design Optimization Can Reduce Manufacturing Complexity
One of the most effective ways to improve an investment casting project is to review the design before tooling.
Leierwo’s manufacturing process includes drawing optimization for wall thickness, fillets and casting feasibility before mold production.
Design improvements may include:
- Reducing unnecessary heavy sections
- Creating smoother wall transitions
- Adding appropriate radii
- Simplifying difficult internal geometry
- Identifying machined surfaces clearly
- Removing unnecessary precision requirements
These changes can improve casting stability and reduce downstream processing.
Wall Thickness
Wall thickness affects both material use and casting behavior.
Very heavy sections consume more metal and cool more slowly.
This can create local hot spots and increase shrinkage risk.
Very thin sections may be difficult to fill reliably.
A well-designed component therefore uses material strategically.
Uniform wall thickness where practical can improve solidification and reduce unnecessary mass.
Part Consolidation
Investment casting can sometimes combine several separate fabricated or machined pieces into one component.
This can reduce:
- Welding
- Fasteners
- Separate inventory items
- Assembly operations
Part consolidation can therefore create value even if the individual casting is more sophisticated.
A purchasing comparison should consider the complete assembly rather than simply compare one casting with one conventional component.
The real question is whether the casting simplifies the total manufacturing system.
Material Waste and Near-Net-Shape Design
Investment casting can reduce material removal because much of the final geometry is produced directly by the mold.
This is particularly valuable for complex stainless or alloy steel components where machining a full part from solid stock would remove substantial material.
Near-net-shape design concentrates machining on critical areas instead.
Leierwo’s investment casting service emphasizes complex geometry capability and reduced downstream processing through better as-cast accuracy and surface finish.
Small Batch vs Mass Production
The most economical manufacturing strategy can change with quantity.
For small batches, manufacturers may favor more flexible processes.
For stable repeat production, additional tooling or fixtures may become worthwhile because they improve efficiency and repeatability.
Leierwo’s broader manufacturing services support projects ranging from small-batch customization to larger-scale production.
Buyers should therefore provide forecast volume rather than only the first order quantity.
How Leierwo Evaluates a Casting Project
Leierwo’s current manufacturing process begins with customer drawings and working-condition requirements.
The technical team evaluates material selection and structural feasibility before optimizing the drawing for casting.
The process then moves through mold development, casting production, heat treatment, CNC finishing, inspection and delivery.
This workflow is important because investment casting cost cannot be calculated accurately from component weight alone.
The entire manufacturing route needs to be understood first.
What Information Is Needed for an Accurate RFQ?
A detailed RFQ allows the manufacturer to provide a more realistic production plan.
Buyers should ideally provide:
- 2D engineering drawing
- 3D CAD model
- Exact material grade
- Production quantity
- Annual forecast
- Critical tolerances
- Heat treatment
- Surface finish
- CNC machining requirements
- Inspection requirements
- Application information
Leierwo’s own quotation workflow asks customers to provide CAD drawings or 3D files together with material, quantity and surface-finish requirements before engineering evaluation.
Providing these details early reduces assumptions during quotation.
Why a Photo Is Not Enough
A photograph may help the manufacturer understand the general appearance of a component, but it does not define engineering requirements.
The supplier cannot accurately determine:
- Dimensions
- Material
- Tolerances
- Wall thickness
- Internal geometry
- Quantity
- Machining
- Heat treatment
from an image alone.
For custom precision casting, engineering data is essential.
A complete drawing package produces a much more meaningful quotation than simply requesting a figure based on appearance.
How to Reduce Investment Casting Cost Without Reducing Quality
The best cost reduction does not come from removing necessary quality controls.
It comes from eliminating unnecessary manufacturing requirements.
Several areas deserve attention.
First, use realistic casting tolerances and machine only critical features.
Second, select the material according to actual operating conditions rather than automatically choosing a more specialized alloy.
Third, choose water glass or silica sol casting according to required accuracy and surface quality.
Fourth, review wall thickness and geometry before tooling.
Finally, provide realistic annual quantity so tooling and production strategy can be planned appropriately.
These decisions reduce complexity while preserving function.
Evaluate Total Manufacturing Cost
Buyers should avoid comparing quotations only through the raw casting value.
A more complete evaluation includes:
| Cost Factor | Why It Matters |
|---|---|
| Tooling | Initial investment and production repeatability |
| Material | Determines raw material and processing requirements |
| Casting process | Affects accuracy and surface finish |
| Yield | Influences total metal consumption |
| Heat treatment | Determines final mechanical properties |
| CNC machining | Completes precision functional features |
| Surface treatment | Supports appearance or environmental protection |
| Inspection | Confirms required quality |
| Production quantity | Distributes tooling and setup effort |
A casting that appears less expensive initially may require substantially more machining.
A more precise casting process may reduce later finishing.
The correct comparison should therefore consider the finished usable component.
Choosing Between Water Glass and Silica Sol
The process choice should begin with the drawing.
If the component is a structural machinery part with moderate tolerance and surface requirements, water glass casting may provide the required functionality.
If the component contains complex stainless steel geometry, tighter dimensional requirements or higher surface-quality expectations, silica sol casting may be more appropriate.
Leierwo uses both technologies specifically so projects can be matched to different balances of precision, surface quality and manufacturing requirements.
This avoids using the highest-precision process where it provides no meaningful engineering benefit.
When Investment Casting Provides the Most Value
Investment casting becomes particularly valuable when a component combines several of the following requirements:
- Complex geometry
- Internal cavities
- Detailed features
- Reduced machining
- Relatively tight dimensional control
- Good surface quality
- Difficult-to-machine materials
In these cases, the process can reduce the number of separate manufacturing operations required to create the final geometry.
The value should therefore be measured against alternative manufacturing routes, not just the casting stage itself.
Conclusion
Investment casting cost is determined by the complete manufacturing route rather than one simple variable.
Tooling, geometry, material, component weight, casting yield, production quantity, tolerance, surface finish, heat treatment, CNC machining and inspection all influence the final project requirements.
The most effective way to control these factors is through early engineering collaboration.
A component designed around realistic casting tolerances, appropriate materials and clearly identified machined surfaces can often be produced more efficiently than a drawing containing unnecessary precision or overly complex geometry.
Leierwo’s investment casting capabilities combine water glass and silica sol casting with material selection, structural optimization, mold development, trial production, CNC machining and inspection. This allows the complete production route to be evaluated before repeat manufacturing begins.
FAQ
What has the biggest impact on investment casting cost?
There is no single factor for every component. Material, geometry, tooling, production quantity, tolerance, machining and inspection all affect manufacturing requirements. Complex components with tight tolerances and extensive secondary processing generally require more manufacturing effort.
Is silica sol casting more expensive than water glass casting?
Silica sol casting generally involves higher process requirements but provides better dimensional accuracy and surface quality. Leierwo reports approximately CT4–CT6 and Ra 6.3 for silica sol compared with CT7–CT8 and Ra 12.5 for water glass casting. The correct process should be selected according to actual component requirements.
Does a larger order reduce investment casting cost?
Higher production quantities can distribute tooling and setup effort across more components. They can also allow the manufacturer to optimize material purchasing, fixtures and production scheduling. The actual benefit depends on the specific project and manufacturing route.
Does CNC machining significantly affect the finished casting cost?
It can. Components requiring multiple precision bores, sealing surfaces, threads or complex machining setups require more downstream processing. Designing the casting close to final shape and machining only critical features can reduce unnecessary material removal.
How can I receive a more accurate investment casting quotation?
Provide complete 2D drawings and 3D CAD files together with the exact material grade, quantity, critical tolerances, heat treatment, surface finish, machining and inspection requirements. Leierwo uses these details to evaluate the actual manufacturing process before preparing a project quotation.
Product Categories
- Valve Parts
- Water Pump Parts
- Bearing Box Parts
- Die Casting Parts
- Stainless Steel Pump Products
- Cast Iron Pump Products
- Valve Parts For Automobile Use
- Auto Parts
- Valve Parts For Civil Use
- Vacuum Pump Parts KF

Let’s start your next project!
Start Your Project with Leierwo
1. Submit Your Inquiry
2. Cost Calculation
3. Start Production
4. Arrange Delivery
FAQ
Yes, we have extensive experience in international trade and can assist customers with export customs clearance and shipping arrangements. We offer various trade terms such as FOB, CIF, and DDP to accommodate different logistics needs.We accept various international payment methods, including T/T (Telegraphic Transfer), wire transfer, and Letter of Credit (L/C). Payment terms can be discussed with our sales team.
By partnering with Leierwo, you can enjoy competitive pricing and superior quality compared to other suppliers. Additionally, we offer a one-stop solution to deliver finished parts, including CNC machining and surface treatment, ensuring a seamless production process.
We have advanced casting equipment and strict quality control systems. Our monthly production capacity is substantial, and we can manufacture products based on customer-provided drawings or samples. We accept both small trial orders and large-scale production.
Our products comply with international standards such as ASTM, AISI, DIN, and JIS. We can provide material test reports and relevant certifications to ensure product quality meets customer requirements.
We strictly follow the ISO 9001 quality management system and conduct multiple inspections throughout the production process, including spectrographic analysis, X-ray testing, ultrasonic testing, and dimensional measurements. These quality control measures guarantee that our castings meet the highest standards.
Our MOQ depends on the product type and complexity, However, we are flexible and open to discussing your specific needs.
Our standard production lead time is 4-6 weeks, depending on order quantity and product complexity. We strive to shorten delivery times to meet customer demands.
Yes, we can provide samples for quality inspection. Sample costs and shipping fees can be negotiated, and sample fees may be refunded upon placing a formal order.
 English
 Spanish
 Arabic
 Malay
 German